The problem
Vibration monitoring is a mature discipline and dedicated analysers do it far better than this system does. What those analysers usually are, in a small or mid-sized plant, is a handheld instrument somebody walks round with monthly — if the round happens.
The gap is not analytical depth. It is continuity, and it is correlation. A monthly reading cannot see a bearing that started to degrade three weeks ago, and a vibration-only instrument cannot see that the housing is also running warm and the acoustic signature has changed, which together mean something quite different from vibration alone.
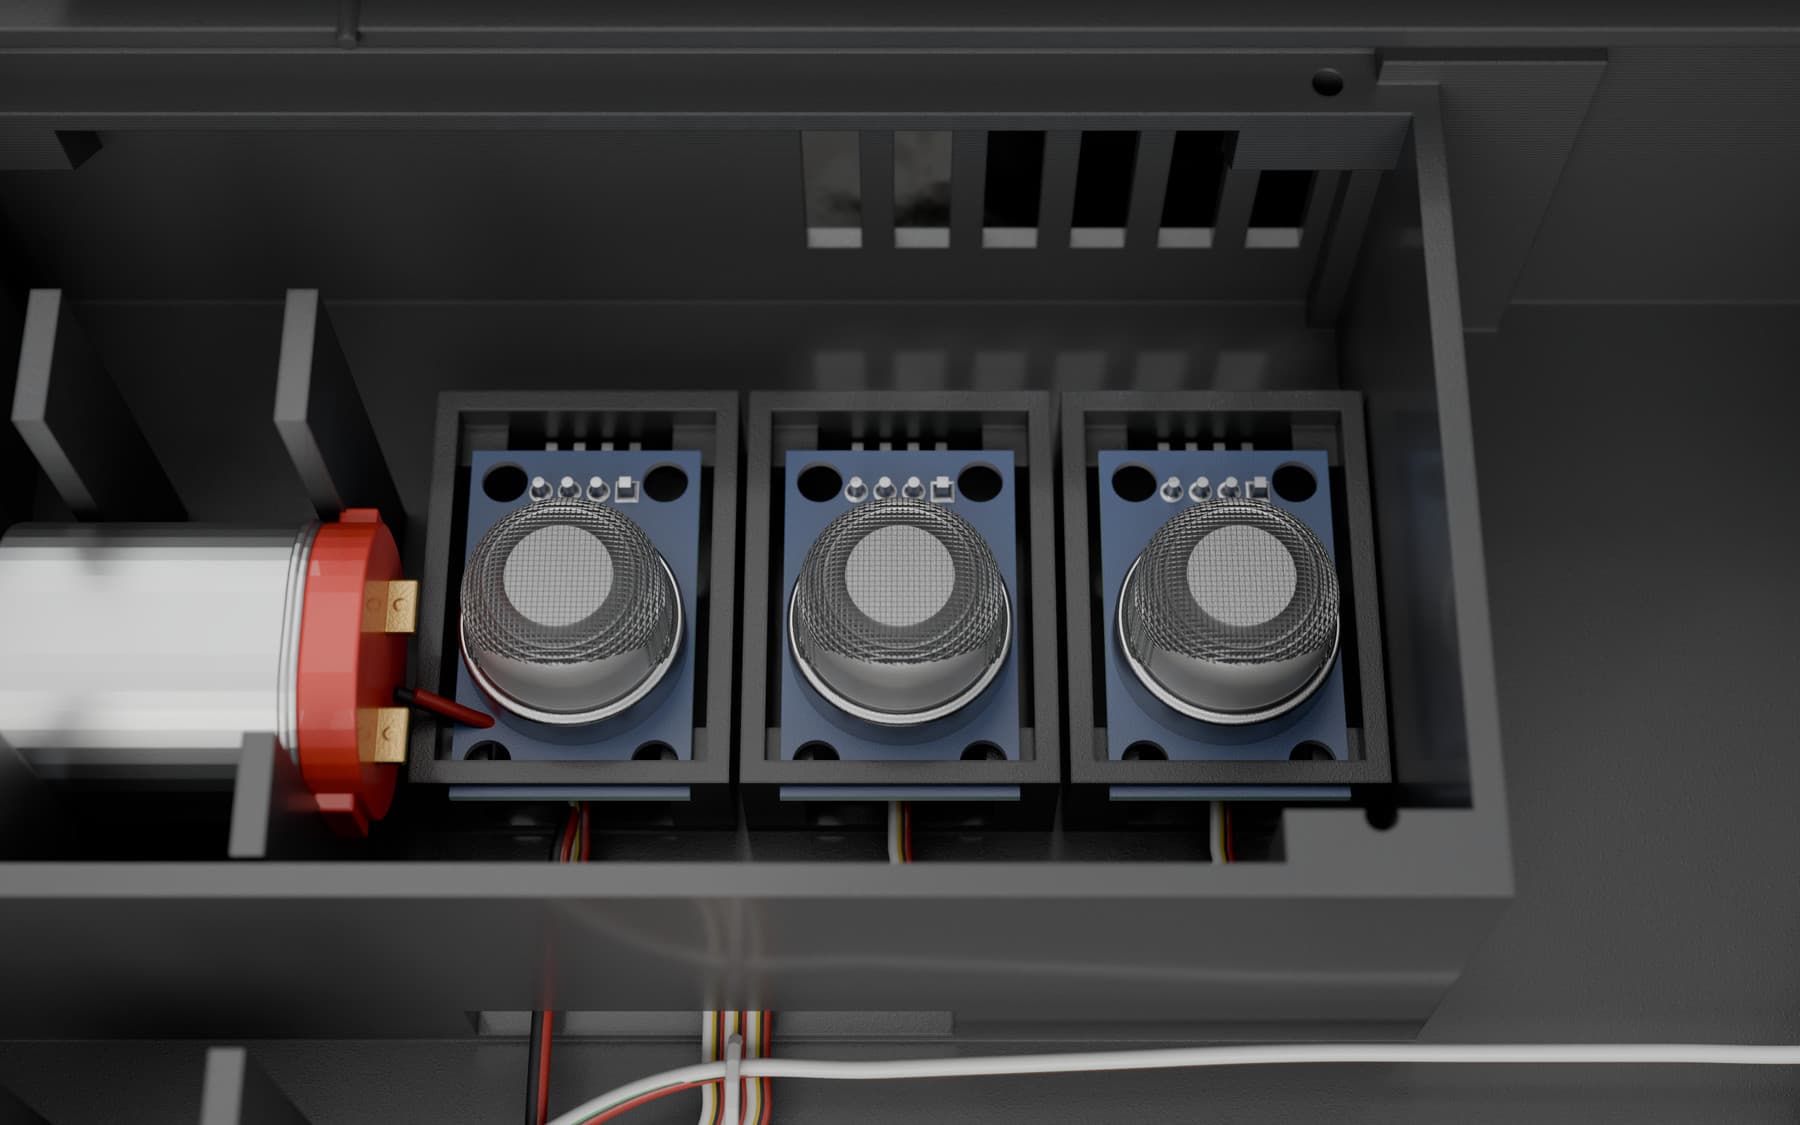
Which channels see it
Detection here is not one sensor reporting a number. It is several channels read at the same instant, where what one channel does NOT do is often as informative as what another does.
- Vibration — A three-axis inertial channel. Both magnitude and its variability matter — increasing jitter is often the earlier signal.
- Sound level — Mechanical noise rises with degradation. A FALL on this channel means something has stopped, which is its own alarm.
- Surface temperature — A contact probe on the housing. Friction becomes heat before it becomes failure.
- Ambient temperature — The reference. A housing warming while the room does not is the machine, not the weather.
- Combustible gas — Its absence separates mechanical degradation from a process event happening nearby at the same time.
How it is detected
The mechanical-degradation signature is vibration magnitude and jitter increasing, acoustic level rising, and the housing warming — with no gas signature. That last clause matters: it is what stops a solvent event near a pump being classified as a failing pump.
Because the node samples continuously rather than on a monthly round, the useful measure is the trend against that machine's own established baseline rather than an absolute threshold. Every machine has its own normal; what is diagnostic is departure from it.
Ventilation failure is the mirror image and is detected the same way. When an extraction fan stops, the acoustic channel FALLS, and humidity and temperature then drift up together. A rising-threshold instrument has no vocabulary for a channel going down; a derivative one treats a negative velocity as exactly as informative as a positive one.
What an operator gets
The output is meant to be actionable by somebody on shift, not interpreted by an engineer afterwards.
- Continuous monitoring instead of a monthly round, with the trend visible over weeks.
- Correlation with heat, sound and gas on the same unit at the same instant — which is what turns a vibration reading into a diagnosis.
- A time-to-threshold estimate on the trend, so maintenance can be planned rather than reactive.
- Detection of stoppage as well as degradation: a fan that has stopped is caught by the acoustic channel falling.