The hazards in this environment
Every industry has a characteristic risk profile, and monitoring is only useful when it is aimed at that profile rather than at a generic list.
- Carbon monoxide - Produced continuously by combustion and by carbonaceous mould materials. It is odourless, it accumulates in enclosed and low-ventilation spaces, and it is the most common serious exposure in the industry.
- Extreme radiant heat - A hazard to people and to equipment. It also constrains where anything electronic can be installed.
- Moisture and molten metal - Water contacting molten metal flashes to steam with explosive force. Damp moulds, damp charge material and damp floors are the routine causes.
- Silica and metal dust - A chronic respiratory hazard from sand handling, shakeout and finishing, rather than an acute event.
What to monitor
Which channels matter, and in roughly this order of usefulness for this industry.
- Carbon monoxide - the priority channel in this industry by a wide margin
- Ambient temperature, for thermal load in working areas rather than at the melt
- General air quality, as a proxy for particulate and combustion loading
- Humidity, which is directly relevant given the moisture risk
- Smoke, acknowledging that a foundry has a high smoke background
Where the nodes go
Placement decides whether monitoring works. A node in the wrong place produces confident silence, which is worse than no node at all because it is trusted.
- Charge preparation and material storage, where damp material is the risk being managed
- Enclosed or partly enclosed areas along pouring routes, where CO collects
- Shakeout and finishing, for dust and CO in a space where people work continuously
- Well back from the melt deck, in ambient conditions the enclosure can survive
What prediction adds here
CO accumulation in a partly enclosed space is close to the ideal case for time-to-threshold: the rise is usually gradual, driven by a ventilation balance rather than an event, and a projection gives real notice. Humidity trending upward in a charge store is a different and equally useful signal - it is a leading indicator of the moisture problem rather than a consequence of it.
What Alfa HazardX covers today
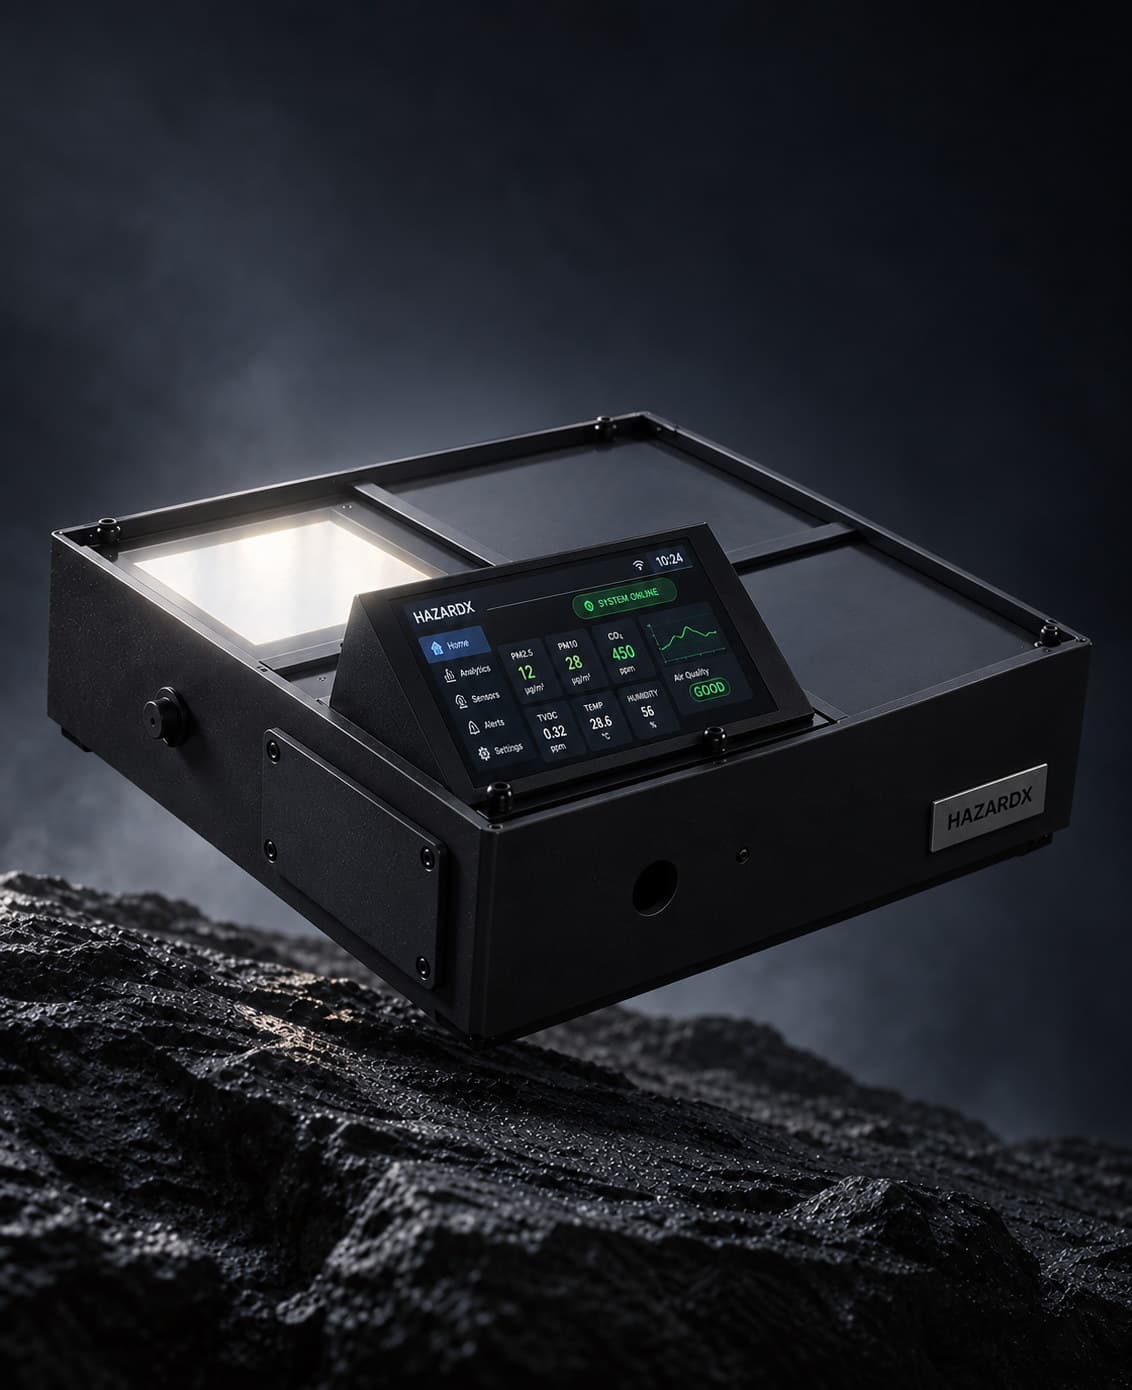
Alfa HazardX covers CO, ambient temperature, humidity, air quality and smoke, with local alarm and time-to-threshold forecasting on the CO channel.